舞阳钢铁S355J2+N热轧钢板质量证明书 - 河钢集团订货
页面头部
热轧钢板质量证明书
QUALITY CERTIFICATE FOR HOT ROLLED STEEL PLATE
主内容容器
第1页内容
基本信息区
订货单位 / CUSTOMER
河钢集团有限公司
生产单位 / PRODUCTION UNIT
舞阳钢铁有限责任公司(WUYANG IRON AND STEEL CO.,LTD.)
合同编号 / CONTRACT NO
J590**7002
证明书号 / CERTIFICATE NO
B105A13096J590217002
牌号 / GRADE
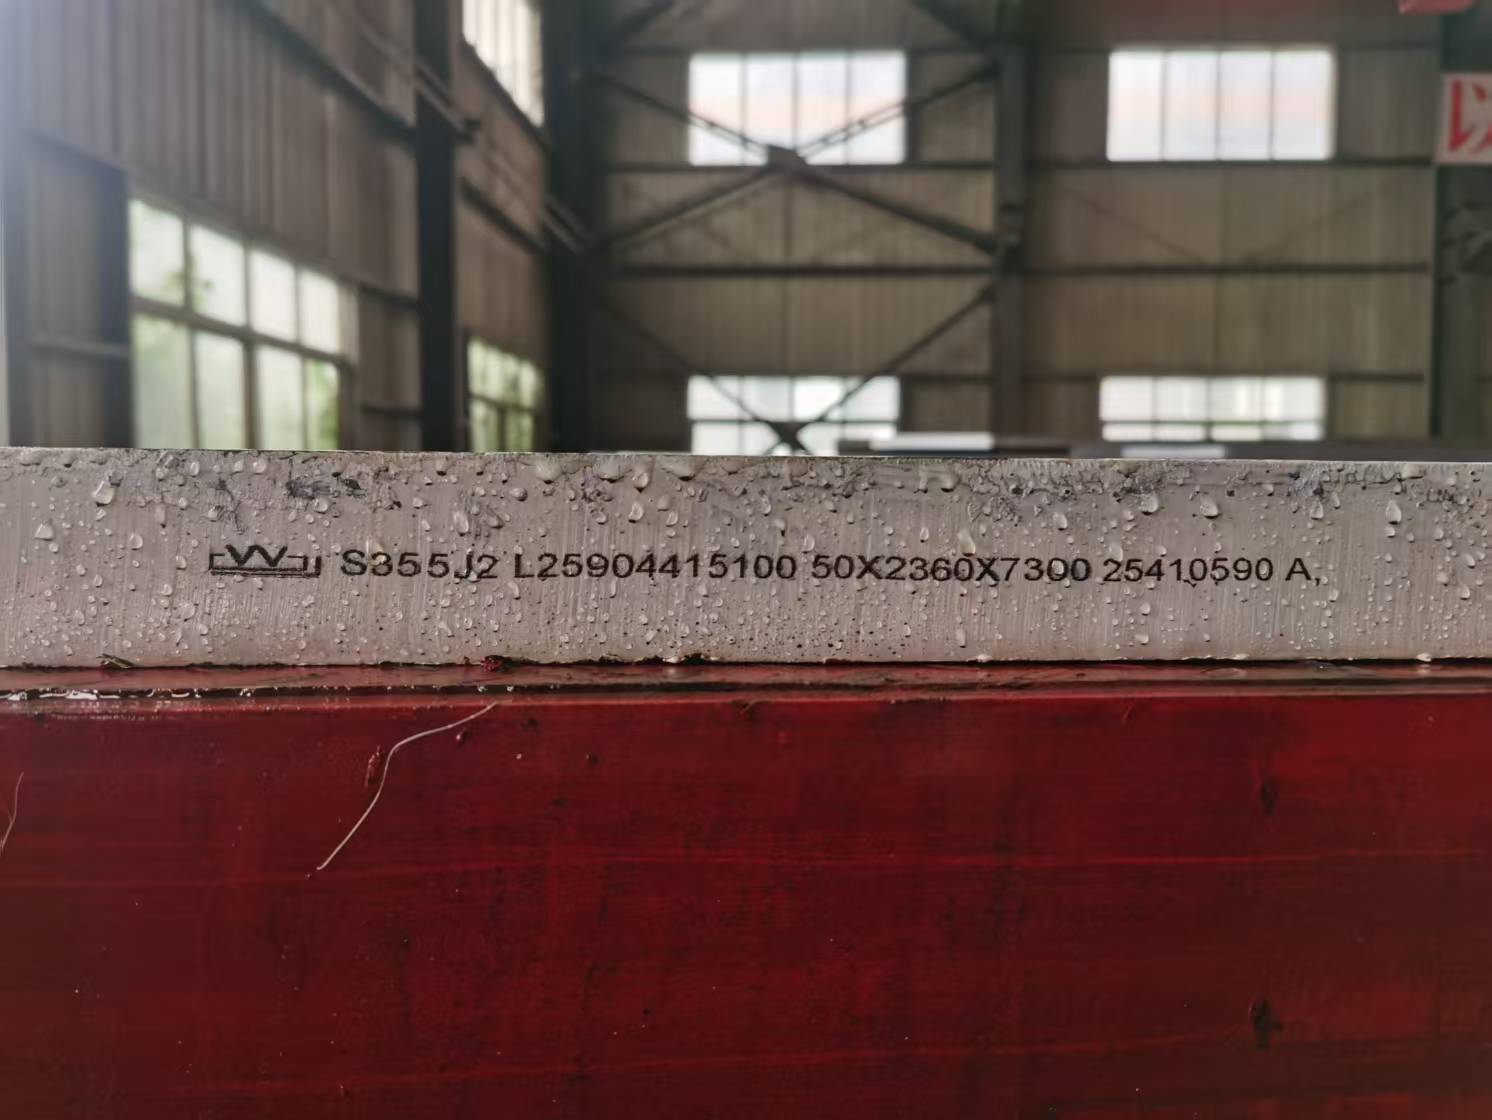
S355J2+N
产品名称 / PRODUCT
热轧钢板(HOT ROLLED STEEL PLATE)
供货状态 / CONDITION OF SUPPLY
正火轧制(NORMALIZED ROLLING)
技术条件 / TECHNICAL CONDITION
EN10025-2:2019
生产许可证号 / PROCESS LICENSE NO
CE(0035、0035-CPR-A203)
车号 / TRAIN NO
豫DQ2**挂
出具日期 / CREATE DATE
2025年10月13日
客户服务电话 / SERVICE PHONE
0375-8*
检测数据表格
材料检测数据 / MATERIAL TEST DATA
| 材料号 | 批次号 / BATCH NO. | 熔炼号 / HEAT NO. | 宽度(mm) | 长度(mm) | 重量(t) / MASS | 抗拉强度(MPa) / T.S | 屈服强度(MPa) / Y.S | 超声检测 / ULTRASONIC TEST | 外观尺寸 / VISUAL & DIMENSIONS |
|---|---|---|---|---|---|---|---|---|---|
| L2592***100 | 25105*4 | - | 2200 | 6000 | 6.123 | 符合要求 | 合格(ACCEPTABLE) | ||
| 合计重量 / TOTAL MASS:6.123t | 检测标准:EN10204/3.1 | |||||||||
质量声明
质量声明 / QUALITY STATEMENT
- 1. 本质量证明书符合EN10204/3.1标准要求(Quality certificate in accordance with EN10204/3.1)。
- 2. 特此证明:本证书所述材料已按订单要求及材料规范进行生产和检验,结果符合规定(We hereby certify that the material described herein has been manufactured and tested with satisfactory results in accordance with the requirements of the material specification and order terms)。
第2页内容
检测注释说明(1)/ TEST NOTES (1)
*1 化学分析 / Chemical Analysis
- 0:熔炼分析(Ladle analysis)
- 1:成品分析(Product analysis)
*2 试样位置 / Sample Location
- T:头部(HEAD) | B:尾部(TAIL)
- 1:钢板角部(a corner of the plate)
- 2:钢板板宽1/4位置(1/4 width from the longitudinal edge of the plate)
- 3:钢板板宽1/2位置(1/2 width from the longitudinal edge of the plate)
- 4:钢板距离板边200mm位置(200mm from the longitudinal edge of the plate)
- 5:钢板板宽3/4位置(3/4 width from the longitudinal edge of the plate)
- 7:钢板板宽1/3位置(1/3 width from the longitudinal edge of the plate)
*3 试样状态 / Condition of Test Piece(续下页 / To be continued on next page)
- p:正火+回火+最大模拟焊后(Normalized+Tempered+Max simulative PWHT)
- q:正火+回火+最小模拟焊后(Normalized+Tempered+Min simulative PWHT)
- [: 正火+最大模拟焊后(Normalized+Max simulative PWHT)
- ]: 正火+最小模拟焊后(Normalized+Min simulative PWHT)
- e:热成型+正火+最小模拟焊后(Thermoforming+Normalized+Min simulative PWHT)
- g:回火+模拟焊后(Tempered+Simulative PWHT)
- i:正火+正火+模拟焊后(Normalized+Normalized+Simulative PWHT)
- s:热成型+正火(Thermoforming+Normalized)
- $:淬火+回火(Quenched+Tempered)
- 0:交货状态(Delivery status)
- 1:最大模拟焊后(Max simulative PWHT)
- 2:最小模拟焊后(Min simulative PWHT)
- 3:调质(Quenching tempered)
- 4:模拟焊后(Simulative PWHT)
- 5:热成型(Thermoforming)
- 6:正火(Normalized)
- 7:回火(Tempered)
- 8:淬火(Quenching)
- 9:正火+回火(Normalized+Tempered)
*4 试验方向 / Test Piece Orientation
- L:纵向(Longitudinal)
- C:横向(Transverse)
- Z:Z向(Through-thickness)
*5 屈服类型 / Yield Strength Type
- 2:Rp0.2 | 3:ReL | 4:ReH | 5:Rt0.5 | 6:Re
第3页内容
检测注释说明(2)/ TEST NOTES (2)
*3 试样状态 / Condition of Test Piece(续)
- D:热成型+模拟焊后(Thermoforming+Simulative PWHT)
- E:热成型+最大模拟焊后(Thermoforming+Max simulative PWHT)
- F:热成型+最小模拟焊后(Thermoforming+Min simulative PWHT)
- H:正火+回火+模拟焊后(Normalized+Tempered+Simulative PWHT)
- I:热成型+正火+回火(Thermoforming+Normalized+Tempered)
- P:正火+模拟焊后(Normalized+Simulative PWHT)
- S:热成型+正火+回火+模拟焊后(Thermoforming+Normalized+Tempered+Simulative PWHT)
- V:热成型+正火+模拟焊后(Thermoforming+Normalized+Simulative PWHT)
- X:热成型+正火+回火+最大模拟焊后(Thermoforming+Normalized+Tempered+Max simulative PWHT)
- Y:热成型+正火+回火+最小模拟焊后(Thermoforming+Normalized+Tempered+Min simulative PWHT)
- A:交货态+模拟焊后(Delivery status+Simulative PWHT)
- B:交货态+最大模拟焊后+最小模拟焊后(Delivery status+Max simulative PWHT+Min simulative PWHT)
- Z:交货态+(正火+回火+最大模拟焊后)+(正火+回火+最小模拟焊后)(Delivery status+(Normalized+Tempered+Max simulative PWHT)+(Normalized+Tempered+Min simulative PWHT))
*6 厚内位置 / Position of Specimen
- 0:原厚(Full thickness) | 1:面下1mm(Below the surface)
- 2:面下2mm(Within 2mm from the surface) | 5:面下1.6mm(Below the surface)
- 6:1/4厚度(1/4 of the thickness) | 7:1/2厚度(1/2 of the thickness)
- 8:1/3厚度(1/3 of the thickness) | 9:留一个轧制面,减薄至12mm(Reserve a rolling surface, thinning to 12mm)
- A:上表面三点(The upper surface 3 points) | B:上下表面各三点(The upper surface 3 points and lower surface 3 points)
- C:1/2厚度(1/2 of the thickness) | D:留一轧制面(Reserve a rolling surface)
- J:上下表面、板厚1/4、1/2、3/4各一点(The upper surface, lower surface and thickness of 1/4,1/2,3/4 each of 1 point)
*7 硬度测量位置 / Hardness Test Location
- 0:上表面+下表面(The upper and lower surfaces) | 1:上表面(The upper surface)
- 2:侧面(Side) | 3:1/4厚度(1/4 thickness position) | 4:1/2厚度(1/2 thickness position)
- 5:3/4厚度(3/4 thickness position) | 7:下表面(The lower surface) | 8:1/3厚度(1/3 thickness position)
- 9:全厚(The entire thickness) | A:上表右侧上(On the head end of right side, the upper surface)
- M:全厚度三点(Three points of the entire thickness) | Q:试样上下表面各打3点(3 points at upper surface and 3 points lower surface of the sample)
- X:距离边缘一个厚度位置,钢板4角上下表面各3点(Three points respectively at upper surface and lower surface of four corners with a distance to the edge equal to nominal thickness)
生产单位信息
生产单位信息 / PRODUCTION UNIT INFO
- 单位名称:舞阳钢铁有限责任公司(WUYANG IRON AND STEEL CO.,LTD.)
- 地址:中国河南省舞钢市(WUGANG, HENAN, CHINA)
- 客户服务中心 (CUSTOMER SERVICE CENTER PHONE NUMBER)
- 质量证明书验证:通过舞钢质量证明书下载和自动验证网址查询(Verify via Wuyang Steel certificate download & verify site)
关键词区域
核心关键词 / KEYWORDS
热轧钢板质量证明书
S355J2+N钢板
EN10025-2:2019标准
舞阳钢铁有限责任公司
河钢集团有限公司
正火轧制钢板
CE认证钢板
钢板拉伸试验
钢板超声检测
钢板冲击试验
热轧钢板检测报告
工业用热轧钢板
分页控制
延伸阅读
挑几篇相关的,接着看: